Sponsored article
How to Match Sheet Metal Surface Finishing to the Material and Required Finish
The same sheet metal component may require a completely different surface-finishing approach depending on the manufacturing processes used beforehand. Laser cutting typically produces smooth edges with minimal burrs, resulting in parts that are often close to assembly-ready. Plasma cutting, on the other hand, creates noticeable oxide scale around the perimeter and introduces a significantly larger heat-affected zone into the metal structure. Welding complicates matters further by generating visible heat discolouration along weld seams, particularly on stainless steel components.
Selecting the appropriate finishing strategy requires more than identifying the mechanical defect. It is equally important to consider the physicochemical properties of the material and the requirements imposed by subsequent manufacturing operations.
Processing After Laser Cutting, Plasma Cutting and Welding
Edges produced by laser cutting are generally clean and often require only limited mechanical finishing. The kerf width depends on the cutting source and is typically narrow enough to minimise the volume of molten material generated during the process.
Plasma cutting creates a very different edge condition, producing thick oxide scale and increasing the risk of microcracks near the cut zone. Such residues usually need to be removed with aggressive machining tools before the component proceeds to powder coating or welding operations.
Welding stainless steel introduces another challenge in the form of characteristic blue, yellow and violet heat-tint discolouration. Removing weld discolouration requires exceptional precision so that only the degraded surface layer is removed without unnecessarily affecting the corrosion-resistant passive layer.
Carbon steel generally tolerates mechanical abrasion well, making it suitable for rapid scale removal after oxy-fuel cutting. However, excessive tool pressure may cause secondary overheating and create new oxide layers that reduce coating adhesion.
Stainless steel requires stricter thermal control because local overheating can damage the chromium oxide layer responsible for corrosion resistance. Aluminium presents different challenges due to its low melting temperature and softness. During grinding operations, it can smear across abrasive surfaces and clog abrasive grain spaces.
Since aluminium oxide differs in hardness from the base material, safe processing of light alloys often requires dedicated non-woven abrasives and carefully controlled cooling conditions.
The thickness of the workpiece also affects the finishing strategy. Thin sheets below approximately 2–3 mm are highly susceptible to deformation, making excessive roller pressure or high feed rates potentially problematic. Thicker materials, particularly those above 10 mm, can withstand more aggressive burr removal but place greater demands on spindle power.
The initial edge condition largely defines the machining sequence. Heavy slag accumulations are typically removed first using the most aggressive tooling; sharp edges are rounded with flap-based systems, and decorative satin finishes are produced using dense non-woven finishing rollers.
Machine Parameters, Automation and Dust Extraction
Abrasive grain size, vertical tool pressure and conveyor speed all influence the final surface roughness, which is often a critical parameter for quality control.
Coarse abrasive grades such as P60-P80 efficiently remove larger material excesses but leave visible directional scratches. Finer abrasives in the P120-P220 range create a more uniform satin finish and increase the effective surface area for adhesive or coating applications.
Excessive rotational speed or excessive pressure inevitably leads to local heat accumulation. On stainless steel, this may appear as brown overheating marks, while aluminium can suffer from embedded molten particles becoming pressed into the surface.
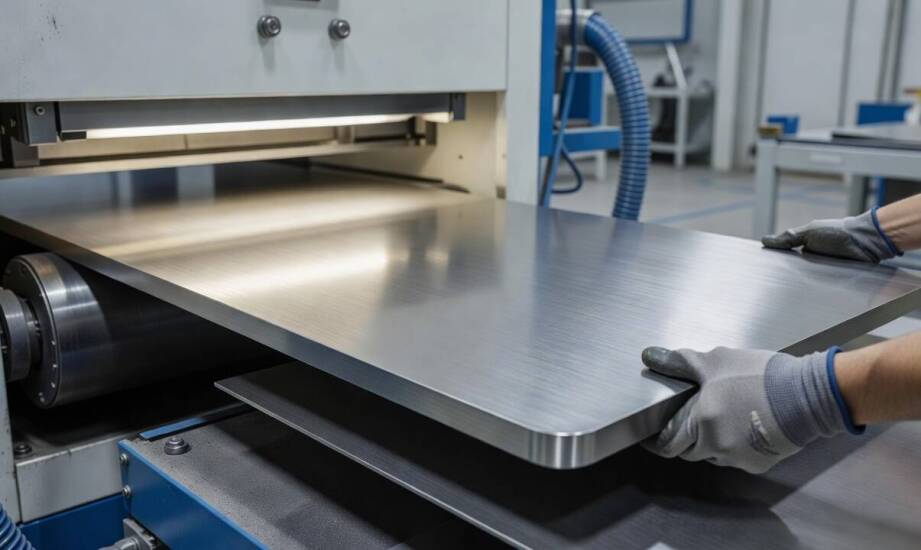
Moving from handheld tools to automated conveyor-based systems stabilises critical process variables. Continuous sheet metal grinding in pass-through machining centres enables simultaneous surface cleaning and edge rounding in a single operation, delivering consistent results across thousands of identical components.
Modern processing units equipped with pneumatic pressure systems maintain consistent contact between the tooling and the workpiece while compensating for minor sheet irregularities.
Madora has implemented a modular design concept in its GP and GL machine series, allowing tool configurations to be adapted to specific cutting technologies and product requirements. This approach reduces reliance on manual processing while supporting the level of consistency required in demanding industries such as automotive manufacturing and aerospace production.
Efficient extraction of metallic dust is an integral part of the production environment and contributes to the reliable operation of multi-tool machining heads.
Properly designed filtration systems immediately remove detached particles from the machining area, preventing debris from becoming trapped beneath pressure rollers and causing secondary scratches.
Dust extraction systems also help protect personnel from airborne particulate matter, improving workplace safety and hygiene. When mechanically processing aluminium or magnesium alloys, wet dust separation systems are commonly used to reduce risks associated with combustible dust generated during intensive machining.
Achieving the Right Surface Finish
Developing an optimal finishing strategy requires analysing the properties of the metal, the nature of defects generated during thermal cutting and the requirements of downstream fabrication processes.
Spindle parameters, abrasive selection, conveyor speed and extraction-system efficiency are all interconnected variables. Understanding these relationships and implementing them within automated pass-through production lines makes it possible to achieve the required edge quality while minimising the risk of thermal damage or deterioration of corrosion-resistant surface layers.
You might be interested
What are pork inner cheeks used for in gastronomy?
What are White Label Supplements?
Which materials are best suited for the production of anti-slip mats?